Views: 11 Author: Site Editor Publish Time: 2026-09-15 Origin: Site
The Critical Role of Surface Finish in Seamless Stainless Steel Tubing for Hydraulic Fittings
In high-pressure hydraulic systems, engineering teams spend significant resources selecting the correct alloy grades, calculating wall thicknesses, and verifying burst pressures. However, a single critical variable is frequently overlooked until a system failure occurs: the surface finish of the seamless stainless steel tube.
The exterior micro-texture of a metal tube directly dictates how effectively a hydraulic adapter can grip, bite, or seal against the outer diameter (OD) wall. Choosing the incorrect specification creates sub-surface pathways for expensive fluid loss.
This comprehensive technical guide evaluates the primary industrial surface finishes for seamless hydraulic tubing, analyzes their compatibility with high-performance stainless steel hydraulic fittings, and explains how to prevent catastrophic "weeping" leaks.

Table of Contents
Why Tubing Surface Roughness Dictates Hydraulic Integrity
The 3 Engineering Surface Finishes for Hydraulic Tubing
2.1 Bright Annealed (BA) — The Gold Standard
2.2 Annealed & Pickled (AP) — The Industrial Baseline
2.3 Electropolished (EP) — The Specialized Purity Choice
Critical Sourcing Warning: Avoid Mechanically Polished Tubing
Comprehensive Fluid System Compatibility Matrix
Protect Your Investment with Fitsch Matching Hardware
1. Why Tubing Surface Roughness Dictates Hydraulic Integrity
When a hydraulic system runs at operational pressures exceeding 315 bar (4,500 psi), fluid particles will aggressively exploit any structural vulnerability. In a typical bite-type fitting assembly (such as DIN 2353 / ISO 8434-1 cutting rings), the sealing integrity relies entirely on a cold-formed metal-to-metal barrier.
If the tube’s exterior surface exhibits microscopic peaks and valleys, the fitting's hard internal cutting edge cannot bridge those gaps uniformly. This leaves microscopic tunnels through which hydraulic oil can slowly escape under intense pressure surges and system vibrations. Engineers measure this texture using Ra (Roughness Average). To guarantee a reliable seal, selecting the appropriate manufacturing treatment is essential.
[ High-Roughness Surface Finish ] ──> Creates Micro-Gaps ──> High-Pressure Fluid Weeping / Leaks
[ Bright Annealed (BA) Finish ]   ──> Uniform OD Seating ──> Zero-Leak Metal-to-Metal Seal (Fitsch Standard)
2. The 3 Engineering Surface Finishes for Hydraulic Tubing
2.1 Bright Annealed (BA) — The Gold Standard
Bright Annealing represents the premier processing specification for precision fluid lines. The seamless tube is induction-heated inside a completely oxygen-free, controlled atmosphere—typically composed of pure hydrogen or dissociated ammonia—and subsequently subjected to rapid cooling.
Surface Profile: Mirror-like, highly reflective, scale-free, and glassy-smooth.
Surface Roughness: Ra ≤ 0.4 μm
Hydraulic Fitting Match: Excellent. This is the definitive finish specified for bite-type metric fittings, twin-ferrule compression systems, and JIC 37-degree flare configurations. Because the outer diameter is uniformly smooth, a Fitsch cutting ring can easily glide into position and bite into the metal smoothly around the entire 360-degree circumference. This eliminates the micro-gaps that cause pressure dropouts.
2.2 Annealed & Pickled (AP) — The Heavy Industrial Baseline
Annealed and Pickled tubing serves as the standard commercial baseline across global distribution markets. The material is heated in an open atmospheric furnace, which inherently generates a dark oxide scale layer. To remove this crust, the tubing is soaked in a chemical acid bath (pickling).
Surface Profile: Dull, matte, non-reflective light gray finish.
Surface Roughness: Ra ≤ 2.5 μm
Hydraulic Fitting Match: Acceptable for low-to-medium stress pipelines. AP tubing provides a highly cost-effective option for large-bore structural fluid transport lines and heavy bolted flange configurations. However, the acid etching process can sometimes leave behind uneven micro-pitting. When deploying AP tubing with precision compression sleeves, buyers must require that the mill maintain exceptionally strict OD tolerances to prevent fluid tracking along the surface texture.
2.3 Electropolished (EP) — The Specialized Ultra-High Purity Choice
Electropolishing is an electrochemical process that targets an already bright annealed tube. The tubing is submerged in an electrolytic chemical bath under a live electrical current, essentially shaving away microscopic surface anomalies on a molecular scale.
Surface Profile: Surgical, brilliant, ultra-smooth sheen.
Surface Roughness: Ra ≤ 0.25 μm
Hydraulic Fitting Match: Overkill for standard mechanical loops. EP finished tubing is strictly reserved for high-precision instrumentation loops, aerospace fuel line modules, and critical semiconductor or pharmaceutical gas distribution networks where particle entrapment cannot be tolerated.
3. Critical Sourcing Warning: Avoid Mechanically Polished Tubing
A frequent and costly procurement error involves purchasing mechanically polished stainless tubing (such as Grit 180, 240, or 320 architectural tubes) for high-pressure fluid systems.
While these tubes look bright and clean, their shine is achieved by spinning coarse abrasive belts or sanding wheels against the metal. This action engraves microscopic, directional circumferential scratches all along the tube’s outer diameter. High-pressure hydraulic fluid will travel directly down these tiny sanding lines, bypassing the internal seals of your fittings and causing a permanent, unfixable weeping leak. Mechanically polished tubing must never be utilized for fluid-power hydraulic networks.
4. Comprehensive Fluid System Compatibility Matrix
Manufacturing Designation | Surface Micro-Roughness | Common Fitting Sealing Mechanism | Leak Mitigation Capability |
Bright Annealed (BA) | Ra ≤ 0.4 μm | Bite-Type Sleeves (DIN 2353), O-Ring Face Seals (ORFS), 37° Flares | Maximum Protection (Best for automated assembly lines) |
Annealed & Pickled (AP) | Ra ≤ 2.5 μm | Heavy-Wall Flanges, Threaded Adapters, Welded Systems | Medium Protection (Requires meticulous inspection for micro-pitting) |
Electropolished (EP) | Ra ≤ 0.25 μm | Elastomeric Face Seals, Ultra-High Purity Compression Fitting | Maximum Protection (Specified for trace gas and pure-fluid lines) |
5. Protect Your Investment with Fitsch Matching Hardware
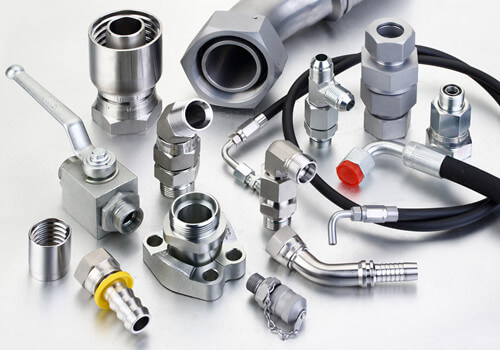
A premium-grade, cold-drawn seamless tube sourced from top-tier mills requires a companion fitting manufactured to identical engineering tolerances. At Fitsch, our complete portfolio of stainless steel hydraulic fittings, adapters, and cutting rings is engineered to seamlessly anchor onto Bright Annealed (BA) and precision Annealed & Pickled (AP) tube walls.
By enforcing rigid geometric compliance and utilizing high-tensile AISI 316L chemical structures, Fitsch components ensure that your tube-to-fitting interface delivers maximum pressure retention, reliable vibration dampening, and total system security.
Don't let a minor surface finish mismatch compromise a complex engineering installation. Visit Fitsch.cn to access complete dimensional CAD profiles, download technical catalogs, or consult our engineering support team to pair your seamless tubing orders with the correct leak-free connection hardware.